
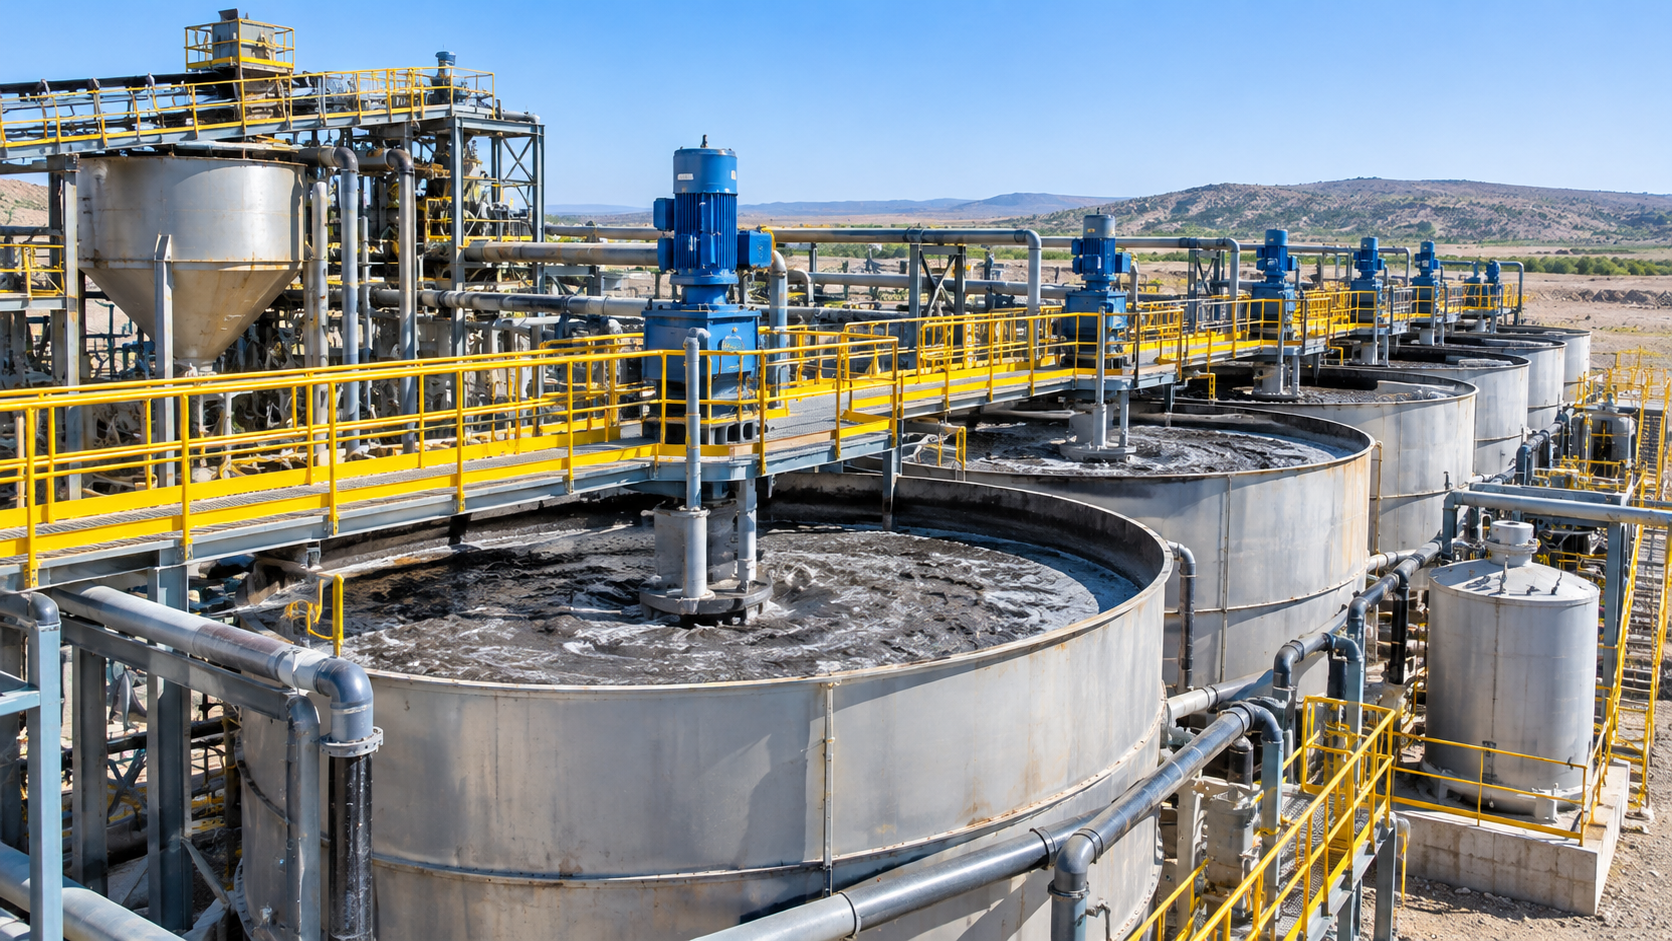
What Are Carbon-in-Leach (CIL) Circuits?
Carbon-in-Leach (CIL) circuits are widely used in gold processing plants to recover gold through a process in which cyanide leaching and adsorption onto Granular Activated Carbon take place together or overlap within the same agitated tanks.
In a CIL gold recovery process, gold-bearing ore is crushed and ground to the required particle size before entering the leaching and adsorption circuit. The ore slurry is treated under controlled metallurgical conditions to dissolve recoverable gold into solution.
Unlike Carbon-in-Pulp (CIP), where leaching is generally completed before the slurry enters separate adsorption tanks, Carbon-in-Leach (CIL) integrates the two operations. Activated Carbon is present while gold dissolution is taking place, allowing dissolved gold-cyanide complexes to be adsorbed as they become available.
The Activated Carbon particles gradually accumulate gold and are subsequently separated from the slurry for elution and downstream gold recovery.
Successful CIL operation depends on ore characteristics, cyanide leaching conditions, oxygen availability, adsorption activity, carbon movement, screening efficiency and the overall design of the processing circuit.
Why Is Activated Carbon Used in CIL Gold Recovery?
Activated Carbon plays a central role in CIL gold recovery by adsorbing dissolved gold-cyanide complexes directly from the ore slurry while leaching is taking place.
Its highly developed internal pore structure provides adsorption sites where dissolved gold species can be retained. This enables gold to be concentrated onto carbon particles that can be physically recovered and processed.
Coconut Shell Activated Carbon is commonly used in gold recovery applications because suitable grades can provide a combination of gold adsorption activity, mechanical hardness and resistance to physical degradation.
In Carbon-in-Leach (CIL) circuits, Activated Carbon supports:
- Adsorption of dissolved gold-cyanide complexes during leaching
- Concentration of dissolved gold onto recoverable carbon particles
- Continuous gold adsorption as leaching progresses
- Recovery of gold-loaded carbon through screening systems
- Transfer of loaded carbon to elution and downstream recovery
- Repeated carbon use following suitable regeneration
- Controlled gold recovery across multiple adsorption stages
- Reduction of soluble gold losses when circuit conditions are properly managed
The selected Activated Carbon must perform reliably under the chemical, mechanical and hydraulic conditions present in the CIL circuit.
How Do Carbon-in-Leach (CIL) Circuits Work?
A typical Carbon-in-Leach process combines gold leaching and carbon adsorption in a series of agitated tanks. The complete circuit includes ore preparation, leaching, adsorption, carbon recovery, elution, regeneration and downstream gold recovery.
Step 1 - Ore Preparation and Grinding
Gold-bearing ore is crushed and ground to achieve the required mineral liberation. The prepared material is mixed with water to form a slurry suitable for processing.
Ore mineralogy, particle size and slurry characteristics influence both the leaching process and subsequent adsorption performance.
Step 2 - Slurry Transfer to CIL Tanks
The prepared slurry enters a series of agitated CIL tanks. Depending on the circuit design, the slurry may undergo preliminary conditioning or partial leaching before contacting Activated Carbon.
The tanks are designed to maintain appropriate slurry mixing, chemical conditions and carbon suspension.
Step 3 - Simultaneous Gold Leaching and Adsorption
Within the CIL circuit, gold is dissolved into solution through controlled cyanide leaching. At the same time, Granular Activated Carbon adsorbs dissolved gold-cyanide complexes from the liquid phase of the slurry.
This simultaneous or overlapping operation distinguishes Carbon-in-Leach from conventional Carbon-in-Pulp circuits.
Step 4 - Gold Adsorption onto Activated Carbon
Dissolved gold species move toward the carbon surface and enter accessible pores, where adsorption occurs.
Adsorption performance depends on carbon activity, pore structure, solution chemistry, dissolved gold concentration and contact conditions.
Step 5 - Counter-Current Carbon Movement
Many CIL circuits operate with slurry moving through the tanks in one direction while Activated Carbon is transferred between tanks in the opposite direction.
This counter-current arrangement helps maintain an effective adsorption driving force and supports the development of higher gold loading on carbon closer to the slurry inlet.
Step 6 - Loaded Carbon Recovery
Gold-loaded carbon is separated from the slurry using suitable screening equipment and transferred to the elution section.
Effective carbon retention is important because losses of fine, gold-bearing carbon can contribute to unrecovered gold.
Step 7 - Elution and Gold Recovery
During elution, adsorbed gold is removed from the loaded carbon using a suitable industrial stripping system.
The resulting gold-bearing solution is processed through downstream recovery operations, which may include electrowinning and smelting.
Step 8 - Carbon Regeneration and Reuse
Following elution, Activated Carbon may undergo regeneration to restore adsorption activity affected by fouling and repeated operation.
Carbon meeting the required physical and adsorption specifications can then be returned to the CIL circuit.
Gold Adsorption Mechanism in Carbon-in-Leach (CIL) Circuits
The primary role of Activated Carbon in CIL circuits is to adsorb dissolved gold-cyanide complexes as gold is released from the ore during leaching.
Activated Carbon contains an extensive internal pore network that provides surface area for the adsorption of suitable dissolved species.
1. Dissolution of Gold
Under suitable leaching conditions, gold is dissolved from the ore into the liquid phase of the slurry as soluble gold-cyanide complexes.
2. Transport of Dissolved Gold
Dissolved gold species move from the bulk solution toward the external surfaces of Activated Carbon particles.
3. Diffusion into Carbon Pores
Gold-cyanide complexes enter accessible pores within the carbon. Pore accessibility and diffusion characteristics influence the rate of adsorption.
4. Adsorption onto Internal Surfaces
Dissolved gold species are retained through interactions with the internal carbon surfaces. Adsorption behavior is influenced by solution chemistry and the presence of competing dissolved substances.
5. Development of Gold Loading
As leaching and adsorption continue, gold accumulates on the carbon particles. The loading achieved depends on available adsorption capacity, dissolved gold concentration and operating conditions.
6. Carbon Recovery and Elution
When carbon reaches the required loading condition, it is recovered for elution and downstream gold processing.
Both adsorption kinetics and loading capacity are important when evaluating Activated Carbon for CIL applications.
Important Activated Carbon Properties for CIL Circuits
Choosing Activated Carbon for Carbon-in-Leach gold recovery requires consideration of several physical and adsorption characteristics.
1. Gold Adsorption Activity
Gold adsorption activity indicates how effectively Activated Carbon adsorbs dissolved gold from a representative solution under defined testing conditions.
High adsorption activity can support effective gold recovery, but actual plant performance must be validated through suitable testing.
2. Gold Loading Capacity
Gold loading capacity describes the amount of gold that carbon can retain under specified conditions. It is influenced by pore structure, solution chemistry and competing adsorbed substances.
3. Carbon Hardness
Mechanical hardness is particularly important in continuously agitated CIL tanks. Carbon with suitable hardness can better withstand repeated mixing, handling and transfer operations.
4. Attrition Resistance
Attrition can generate fine carbon particles during agitation and transfer. When these particles contain adsorbed gold, their loss can affect overall recovery economics.
5. Particle Size Distribution
Particle size affects adsorption kinetics, carbon screening efficiency, hydraulic behavior and transfer characteristics.
The selected carbon size range must be compatible with the plant's interstage screens and carbon handling systems.
6. Pore Structure
An appropriate combination of pore accessibility and adsorption surface is important for gold adsorption.
Surface area alone does not determine gold recovery performance. Adsorption activity and loading behavior must also be considered.
7. Ash and Impurities
Ash content and other carbon quality parameters should be evaluated according to the specifications required by the gold processing operation.
8. Regeneration Performance
The ability of carbon to retain useful adsorption and mechanical properties after repeated elution and regeneration cycles influences long-term operating economics.
Choosing Coconut Shell Activated Carbon for CIL Gold Recovery
Coconut Shell Activated Carbon is widely used in gold recovery because suitable grades can provide a combination of developed pore structure, mechanical hardness and resistance to attrition.
At Carbure Activated Carbon, premium Coconut Charcoal is processed through physical activation using superheated steam at 1000°C to develop the porous structure of Steam Activated Carbon.
The resulting Activated Carbon can be manufactured and classified according to application-specific adsorption and physical performance requirements.
For Carbon-in-Leach circuits, the evaluation of coconut shell-based Activated Carbon should consider:
- Gold adsorption activity under representative conditions
- Gold loading capacity
- Granular particle size distribution
- Mechanical hardness
- Attrition resistance and fine generation
- Ash and other relevant quality parameters
- Elution characteristics
- Regeneration performance
- Compatibility with existing screening and carbon transfer equipment
Carbure Activated Carbon's gold recovery product range includes GOLD CARB 60 and GOLD CARBURE 55. Current technical specifications and application suitability should be confirmed before product selection.
Factors Affecting Carbon-in-Leach (CIL) Circuit Performance
The performance of Carbon-in-Leach circuits depends on both the properties of Activated Carbon and the design and operation of the gold processing plant.
- Ore characteristics: Mineralogy, gold liberation and the presence of interfering minerals influence leaching and adsorption performance.
- Leaching efficiency: Gold must dissolve into solution before it can be adsorbed onto carbon.
- Dissolved gold concentration: The available concentration influences adsorption loading and concentration gradients.
- Activated Carbon activity: Carbon adsorption characteristics affect the rate of gold uptake.
- Carbon inventory: Sufficient active carbon must be present to support the required adsorption duty.
- Slurry characteristics: Solids concentration and mixing influence contact between slurry and carbon.
- Residence time: Adequate time is required for both leaching and adsorption.
- Solution chemistry: Cyanide concentration, pH, dissolved salts and competing substances influence circuit behavior.
- Carbon fouling: Organic and inorganic substances may reduce available adsorption sites.
- Screen performance: Effective screening retains carbon and helps minimize gold-bearing carbon losses.
- Carbon transfer: Controlled carbon movement supports the required gold loading profile.
- Elution and regeneration: Proper downstream treatment helps maintain useful carbon performance.
- Mechanical degradation: Excessive attrition can increase carbon consumption and fine carbon losses.
Plant operators should evaluate these factors together rather than attributing every recovery problem to Activated Carbon quality alone.
Carbon-in-Leach (CIL) vs Carbon-in-Pulp (CIP) Circuits
Carbon-in-Leach (CIL) and Carbon-in-Pulp (CIP) are established gold recovery processes that use Activated Carbon to adsorb dissolved gold.
The principal difference is how gold leaching and carbon adsorption are integrated within the processing circuit.
| Parameter | Carbon-in-Leach (CIL) | Carbon-in-Pulp (CIP) |
|---|---|---|
| Leaching stage | Leaching and adsorption occur together or overlap | Leaching is generally completed before adsorption |
| Carbon addition | Carbon is present during leaching | Carbon is introduced after the separate leaching stage |
| Adsorbent | Granular Activated Carbon | Granular Activated Carbon |
| Gold recovery mechanism | Adsorption of dissolved gold onto carbon | Adsorption of dissolved gold onto carbon |
| Process arrangement | Combined or overlapping leaching and adsorption duties | Separate leaching and adsorption sections |
| Carbon requirements | Suitable adsorption activity and mechanical properties | Suitable adsorption activity and mechanical properties |
Neither CIL nor CIP is universally superior. The preferred circuit depends on ore characteristics, metallurgical testing, process requirements and overall plant economics.
Common CIL Circuit Challenges and Corrective Focus
1. Carbon Attrition and Fine Generation
Continuous agitation and mechanical handling can cause carbon breakage and generate fine particles.
Carbon hardness, transfer equipment, screening arrangements and handling practices should be evaluated to help minimize carbon losses.
2. Reduced Gold Adsorption Activity
Carbon fouling, competing substances and changes in solution chemistry can reduce adsorption performance.
Testing fresh and regenerated carbon can help identify whether reduced carbon activity is contributing to lower gold recovery.
3. Incomplete Gold Leaching
Inadequate leaching conditions can leave recoverable gold within the ore particles.
Ore characteristics, residence time, reagent conditions and metallurgical test results should be reviewed to identify potential limitations.
4. High Soluble Gold in Tailings
High soluble gold losses can result from incomplete adsorption or other circuit limitations.
Carbon inventory, carbon activity, contact conditions, transfer efficiency and screening should be reviewed alongside leaching performance.
5. Excessive Carbon Consumption
High carbon make-up requirements may indicate mechanical degradation, handling losses or other operational problems.
Evaluating carbon consumption over operating cycles provides a more useful comparison than purchasing price alone.
6. Inconsistent Regeneration Performance
Incomplete elution, fouling or unsuitable regeneration conditions may reduce carbon activity over repeated cycles.
Regeneration practices should be evaluated according to plant-specific technical and safety requirements.
How to Select Activated Carbon for CIL Gold Recovery
Selecting the right Activated Carbon grade is important for maintaining reliable gold adsorption, controlling carbon losses and supporting long-term operating efficiency.
1. Understand the CIL Circuit Requirements
Identify the number of leaching and adsorption stages, ore characteristics, slurry conditions, carbon inventory and operating requirements.
2. Evaluate Gold Adsorption Activity
Compare carbon grades under representative testing conditions to understand gold adsorption kinetics and overall performance.
3. Review Gold Loading Capacity
Evaluate the carbon's ability to retain gold under the solution chemistry and loading conditions expected in the circuit.
4. Check Particle Size Compatibility
Select carbon with a particle size distribution compatible with interstage screens and carbon transfer equipment.
5. Consider Hardness and Attrition Resistance
Choose a grade capable of withstanding the expected agitation, pumping, handling and regeneration conditions.
6. Review Carbon Quality
Check moisture, ash, particle size and other applicable physical and chemical specifications.
7. Assess Elution and Regeneration Behavior
Carbon should be evaluated for its ability to release adsorbed gold during elution and retain useful performance after regeneration.
8. Consider Cost Per Operating Cycle
Evaluate carbon consumption, make-up requirements, gold recovery performance and the economic impact of carbon losses.
9. Conduct Plant-Specific Trials
Laboratory testing and controlled plant trials using representative materials provide a stronger basis for grade selection than relying on one specification value.
Why Choose Carbure Activated Carbon for CIL Circuits?
Carbure Activated Carbon Pvt. Ltd., India, manufactures coconut shell-based Activated Carbon for industrial purification and gold recovery applications.
Using premium Coconut Charcoal and Steam Activation technology, Carbure develops Activated Carbon products intended to meet application-specific adsorption and physical performance requirements.
For gold recovery applications, Carbure offers product options including GOLD CARB 60 and GOLD CARBURE 55.
Important considerations for selecting Carbure Activated Carbon for Carbon-in-Leach circuits include:
- Coconut shell-based Activated Carbon for gold recovery applications
- Application-focused product selection
- Gold adsorption and loading performance considerations
- Granular particle size requirements
- Carbon hardness and attrition resistance
- Carbon handling and screening compatibility
- Elution and regeneration performance considerations
- Technical discussions for industrial and bulk requirements
Customers are encouraged to share their CIL operating conditions and request current product specifications to determine the appropriate carbon grade for their application.
Carbon-in-Leach (CIL) Circuits - Final Thoughts
Carbon-in-Leach (CIL) circuits are an important part of gold processing operations because they combine gold dissolution and Activated Carbon adsorption within the same processing circuit.
The overall success of a CIL circuit depends on effective leaching, suitable gold adsorption, controlled carbon movement, reliable screening and appropriate carbon regeneration.
Activated Carbon selection also plays an important role. Gold adsorption activity, loading capacity, pore accessibility, mechanical hardness, particle size and resistance to attrition can influence operating performance.
By selecting suitable coconut shell-based Activated Carbon and validating its performance through representative testing, gold processing operations can work toward improved adsorption efficiency, controlled carbon consumption and consistent gold recovery.
Frequently Asked Questions About Carbon-in-Leach (CIL) Circuits
A Carbon-in-Leach circuit is a gold recovery process in which cyanide leaching and adsorption onto Granular Activated Carbon occur together or overlap in the same agitated tanks. Gold-loaded carbon is subsequently recovered for elution and downstream processing.
Activated Carbon adsorbs dissolved gold-cyanide complexes as gold is leached from the ore. The gold-loaded carbon is separated from the slurry and processed through elution and downstream gold recovery operations.
Suitable coconut shell-based Activated Carbon grades combine gold adsorption characteristics, mechanical hardness and resistance to attrition, making them useful for gold recovery in continuously agitated CIL tanks.
Carbon-in-Leach combines or overlaps gold leaching and carbon adsorption in the same tanks. Carbon-in-Pulp generally separates gold leaching and carbon adsorption into different process stages.
Hardness and attrition resistance help reduce carbon breakage during agitation, transfer and handling. This can help limit the formation and loss of fine carbon particles carrying adsorbed gold.
Yes. Activated Carbon can be reused after gold elution and suitable regeneration. The number of practical operating cycles depends on carbon quality, fouling, physical losses and circuit operating conditions.
The appropriate carbon grade depends on gold adsorption activity, loading capacity, particle size, hardness, attrition resistance, regeneration behavior and site-specific CIL operating conditions. Representative testing is recommended before final selection.
Possible causes include incomplete leaching, inadequate carbon inventory, reduced adsorption activity, poor carbon transfer, insufficient contact time, screen problems and losses of gold-bearing carbon fines.
Looking for Activated Carbon for Carbon-in-Leach (CIL) Circuits?
Carbure Activated Carbon manufactures coconut shell-based Activated Carbon in India for industrial adsorption and gold recovery applications. Our gold recovery product range can be evaluated for adsorption performance, hardness, particle size, carbon handling requirements and regeneration characteristics in Carbon-in-Leach (CIL) circuits.
Share your CIL circuit requirements, gold adsorption targets, operating conditions and required carbon specifications with Carbure Activated Carbon. Contact our team to discuss GOLD CARB 60, GOLD CARBURE 55 and suitable Activated Carbon options for your gold recovery application.
